Bucket Conveyor | Automatic Vertical Bucket Conveyor Manufacturer, Supplier & Exporter

Product Description
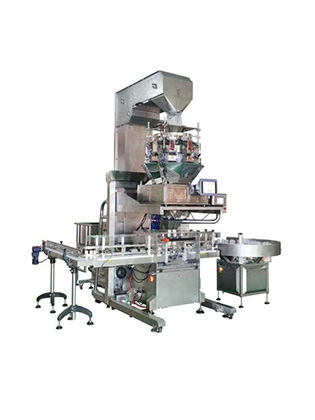
The Bucket Conveyor is a reliable vertical conveying system designed for the continuous lifting and transfer of powders, granules, tablets, capsules, food products and other bulk materials between different levels of a production or packaging line. Also known as a Vertical Bucket Conveyor or Bucket Elevator Conveyor, it provides efficient material handling while minimizing floor-space requirements.
The conveyor uses a series of durable buckets mounted on a continuous belt or chain to collect material from the feeding point and elevate it vertically before controlled discharge at the required height. The system can be customized according to material characteristics, conveying capacity, lifting height and plant layout.
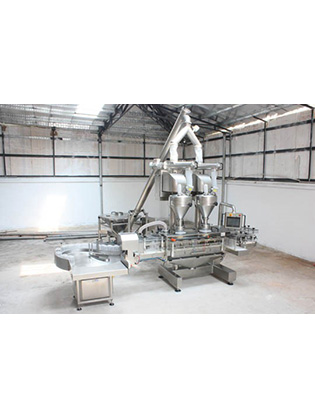
Designed for pharmaceutical, food, nutraceutical, chemical, FMCG and other industries, the Bucket Conveyor Machine can be integrated with weighing systems, filling machines, tablet processing equipment, packaging machines, hoppers, bins and complete automated production lines.
Product Features
- Efficient vertical conveying with minimum floor-space requirement.
- Continuous and controlled material lifting.
- SS304 or SS316 stainless steel construction options.
- Food-grade or industrial-grade buckets available as required.
- Suitable for powders, granules and free-flowing bulk materials.
- Variable-speed operation through VFD control.
- Robust geared motor and drive assembly.
- Easy material feeding and discharge arrangement.
- Adjustable conveying capacity and lifting height.
- Easy-to-clean and low-maintenance construction.
- Can be integrated with automatic production and packaging lines.
- Customized design available according to plant layout and application.
Applications
- Pharmaceutical manufacturing plants
- Nutraceutical and herbal product industries
- Food and snack processing plants
- Powder and granule handling applications
- Chemical processing industries
- FMCG manufacturing and packaging
- Spices and seasoning processing
- Grains, pulses and dry food products
- Tablet and capsule production areas
- Automatic weighing and packing lines
- Material transfer between different production levels
Technical Specifications
| Parameter | Specification |
|---|---|
| Machine Type | Bucket Conveyor / Vertical Bucket Elevator |
| Construction Material | SS304 / SS316 / As per requirement |
| Bucket Material | Food-grade polymer / SS / Engineering plastic |
| Conveying Direction | Vertical / Inclined as per design |
| Capacity | Application and material dependent |
| Lifting Height | Customized as per plant requirement |
| Bucket Size | Customized according to product and capacity |
| Drive | Geared Motor |
| Speed Control | VFD / Variable Speed |
| Control System | PLC / HMI control optional |
| Power Supply | As per customer/site requirement |
| Safety | Emergency stop and protective guarding options |
Working Principle
The Bucket Conveyor operates using a continuous series of buckets mounted on a belt or chain mechanism. Bulk material is fed into the buckets at the bottom loading point. The motor-driven system moves the buckets upward along the vertical conveyor path. Once the buckets reach the discharge point, the material is released into the receiving hopper, machine or process equipment.
The conveying speed, bucket configuration and discharge arrangement can be selected according to the characteristics of the material and required production capacity.
Advantages
- Requires significantly less floor space than conventional horizontal conveying systems.
- Provides efficient vertical transfer of bulk materials.
- Suitable for continuous automated production operations.
- Reduces manual material handling.
- Improves production-line efficiency.
- Can be customized for different capacities and elevations.
- Stainless steel construction provides durability and hygienic operation.
- Easy integration with upstream and downstream machinery.
Optional Features
- SS316 construction for demanding pharmaceutical applications.
- Food-grade bucket configuration.
- Transparent inspection sections.
- Variable-frequency drive system.
- PLC and HMI-based automatic controls.
- Level sensors and product detection sensors.
- Dust-tight enclosure options.
- Customized inlet and outlet hoppers.
- Mobile or fixed mounting arrangement.
- Integration with weighing, filling, packing and processing equipment.
Why Choose Our Bucket Conveyor?
Our Bucket Conveyor Systems are designed to provide dependable vertical material handling for modern processing and packaging facilities. The equipment can be engineered around the required material, capacity, lifting height and available plant space. Stainless steel construction, customized bucket arrangements and automated controls make the system suitable for hygienic and industrial applications.
As an experienced Bucket Conveyor Manufacturer, Supplier and Exporter, we provide customized material-handling solutions for pharmaceutical, food, nutraceutical, chemical, FMCG and allied industries.
Frequently Asked Questions
What is a Bucket Conveyor?
A Bucket Conveyor is a vertical material handling machine that uses a series of buckets to lift and transfer bulk materials from a lower level to a higher level.
What materials can be conveyed using a Bucket Conveyor?
It can be designed for powders, granules, tablets, capsules, grains, spices, dry food products and other suitable bulk materials depending on the bucket design.
Can the Bucket Conveyor be customized?
Yes. Capacity, lifting height, bucket size, construction material, inlet and outlet configuration, drive system and controls can be customized according to the application.
Is the Bucket Conveyor suitable for pharmaceutical applications?
Yes. Stainless steel construction and suitable hygienic bucket configurations can be provided for pharmaceutical, nutraceutical and other controlled manufacturing environments.
Can it be integrated with other machines?
Yes. The Bucket Conveyor can be integrated with hoppers, weighing systems, filling machines, processing equipment, packaging machines and automated production lines.
Call To Action
Looking for a reliable Bucket Conveyor Machine for vertical material handling? Contact us for a customized solution based on your product, capacity, lifting height and production-line requirements. We provide Bucket Conveyor manufacturing, supply and export solutions for pharmaceutical, food, nutraceutical, chemical and FMCG industries.
```